A drawer box — a rigid sleeve sliding over a fitted tray with a ribbon pull — reads as a step up from a folding carton. But the premium feel is not decorative; it comes from controlled tolerances in greyboard cutting, V-grooving, wrapping, and the gap between sleeve and tray. This article walks through how Shenzhen CKT Print builds a 50 ml men's fragrance drawer box in production: the materials, the print and decoration sequence, the assembly, and the QC checks that keep thousands of units consistent.
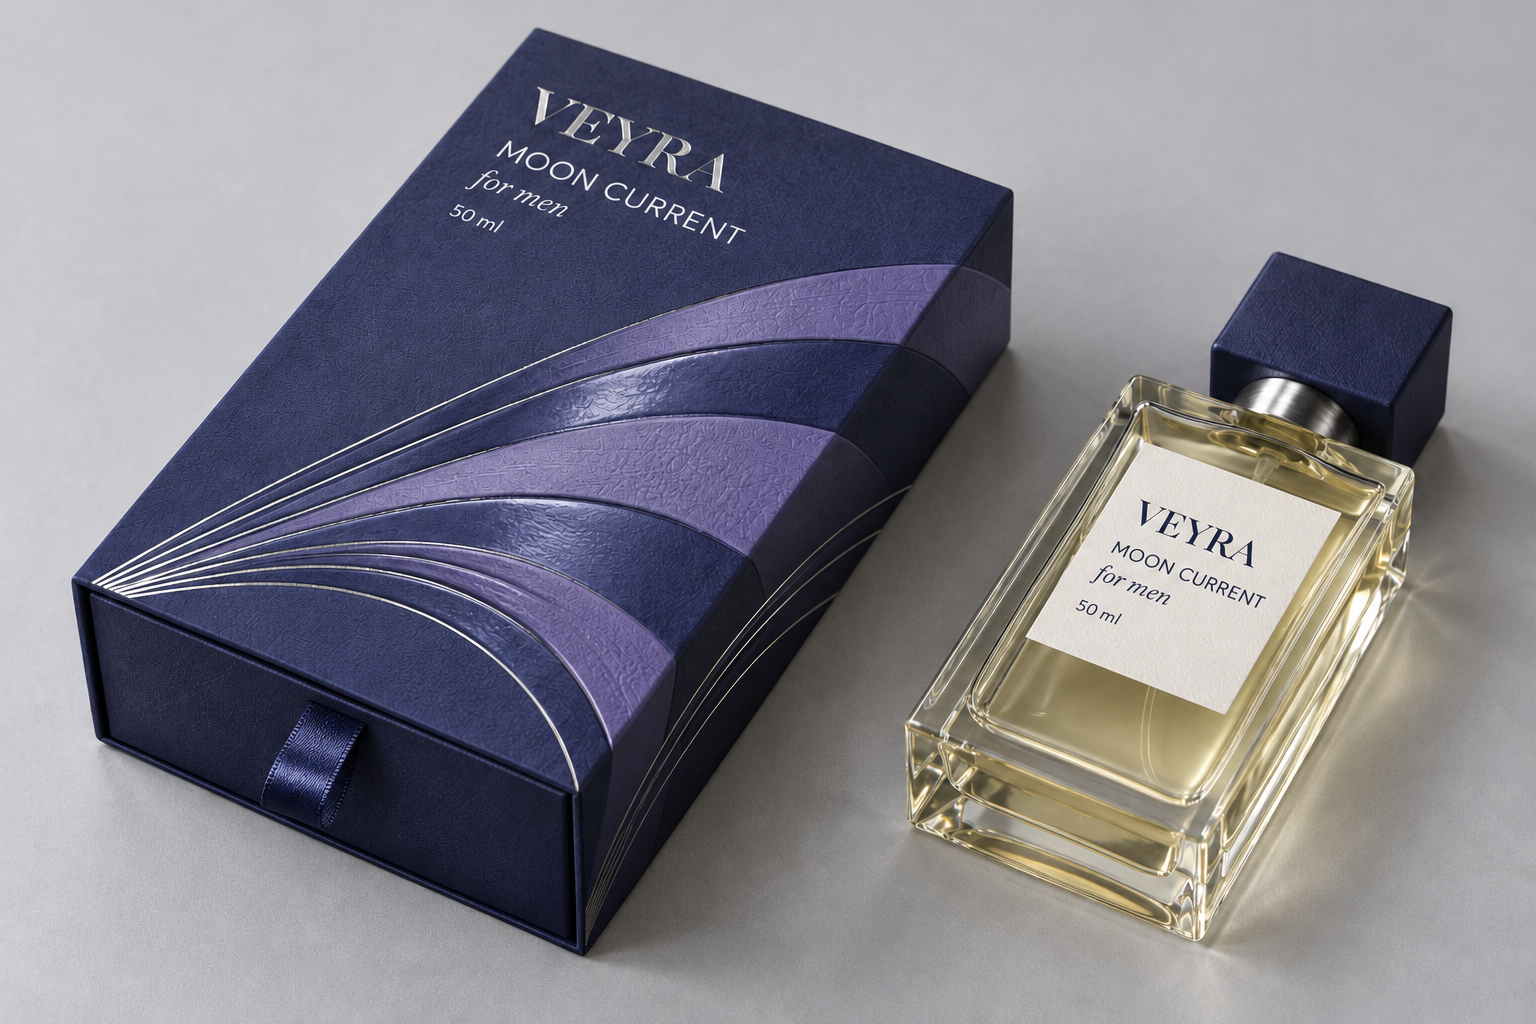
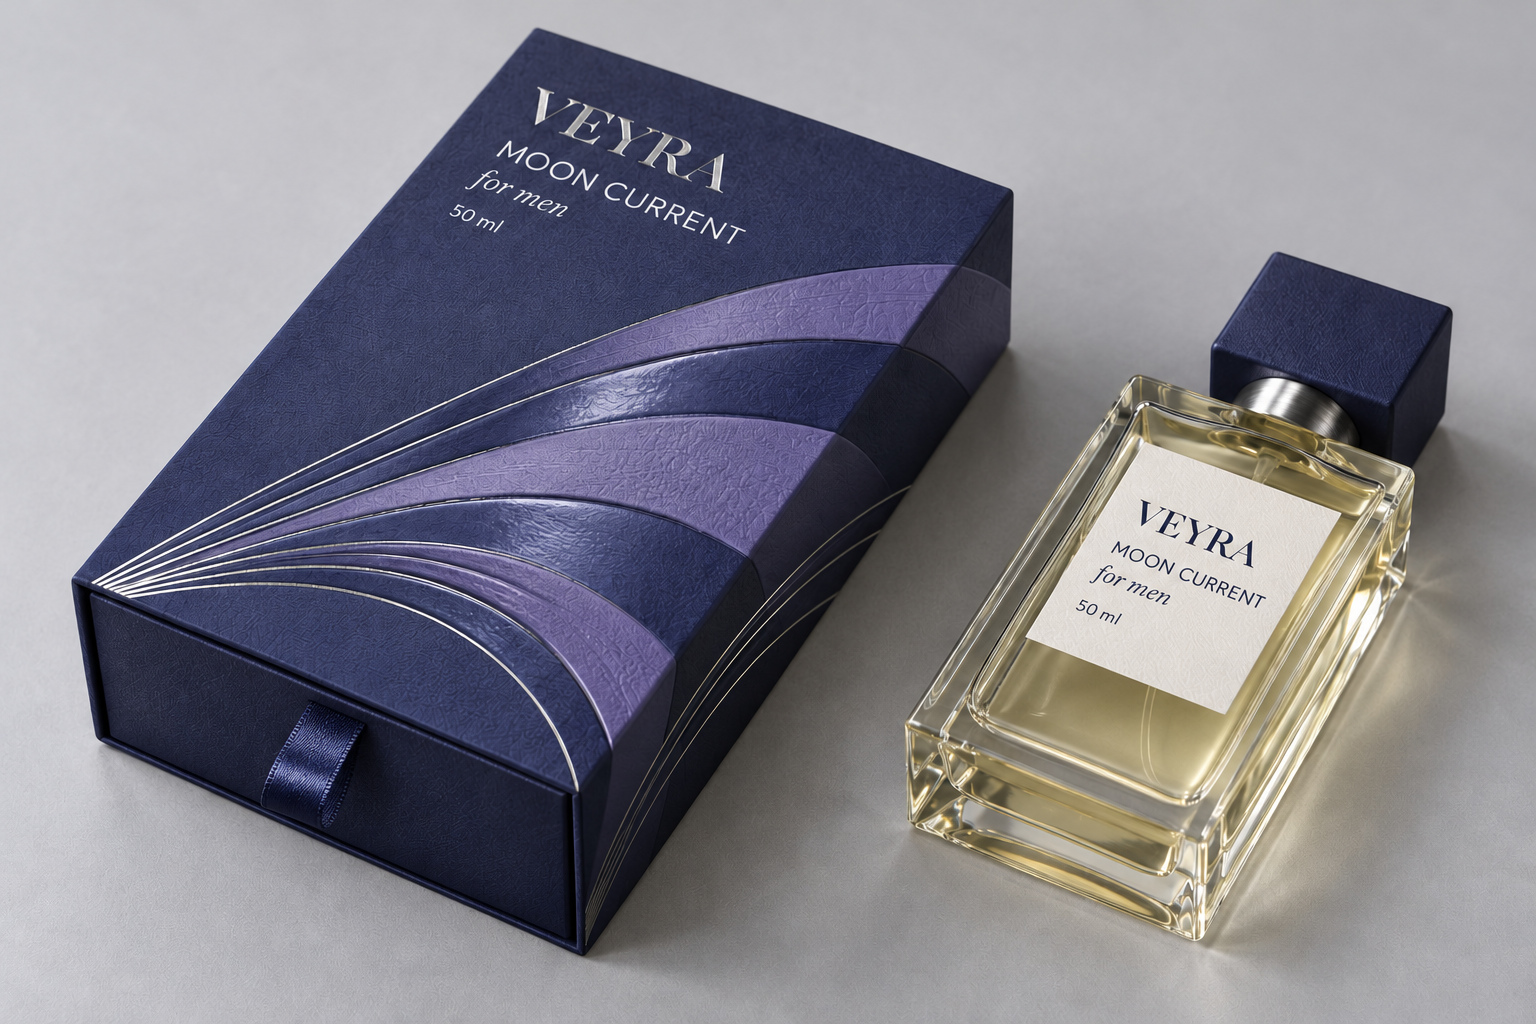
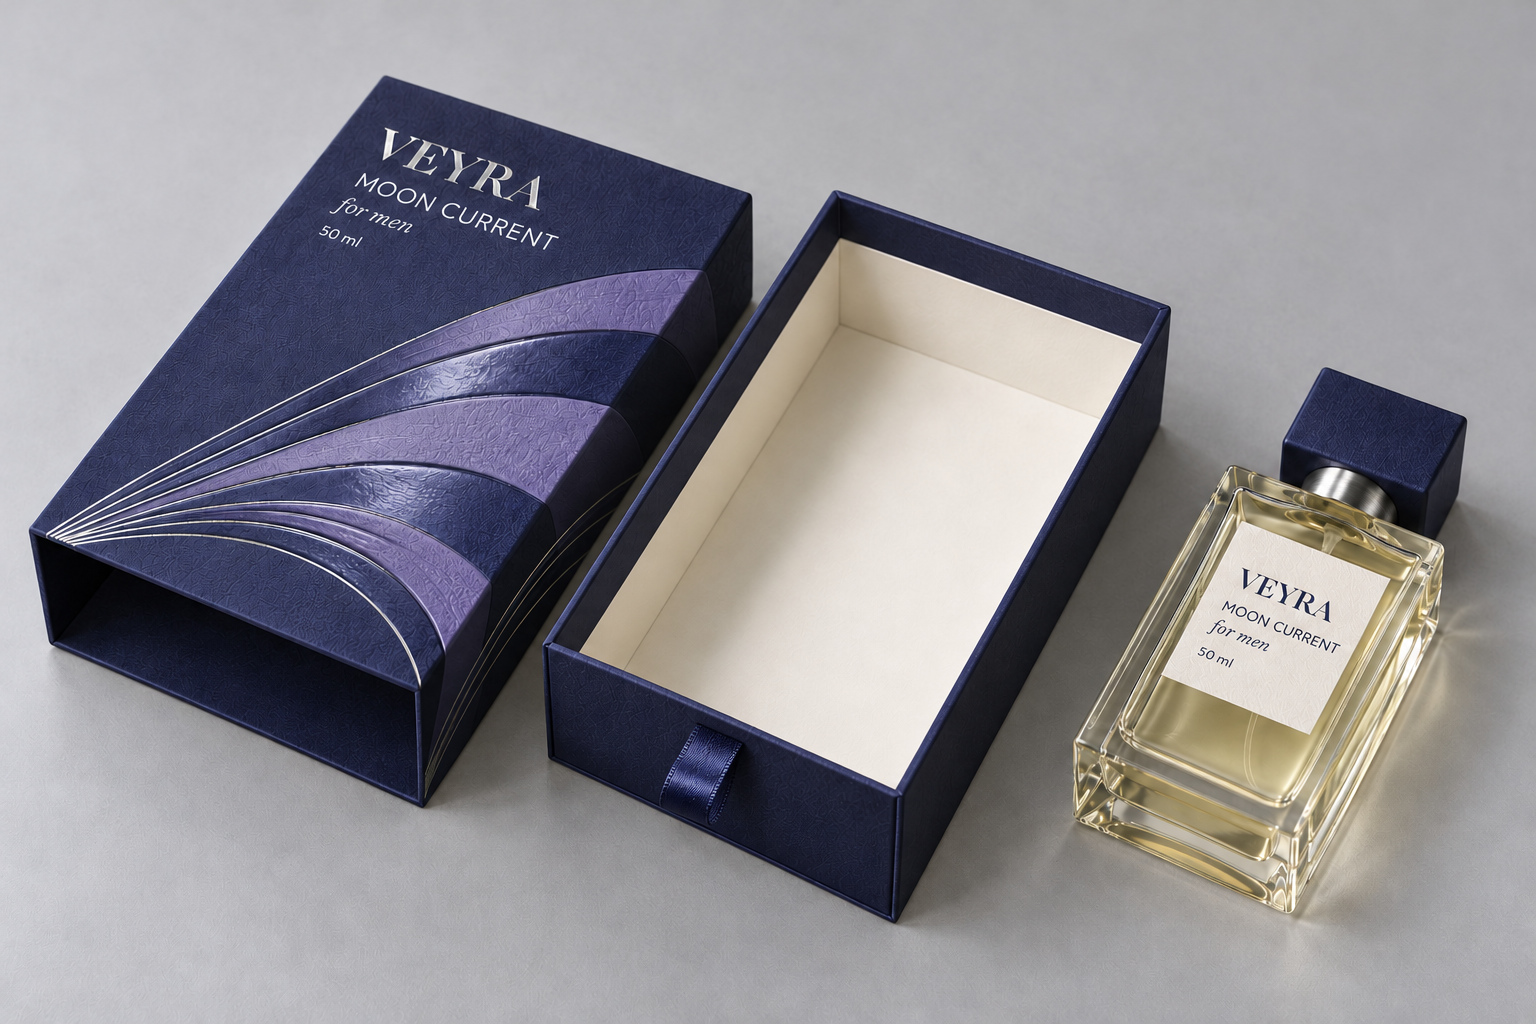
VEYRA Moon Current for men 50 ml — navy textured rigid drawer box with purple fan print, silver foil lines and spot UV.
1. Greyboard Opening and V-Grooving: Why a Drawer Box Needs Two Parts
A rigid drawer box is not one piece. It is a telescoping sleeve that wraps around a tray that slides inside. Both parts start from greyboard (also called chipboard or paperboard), typically 1200–1500 gsm for a 50 ml fragrance box.
The sleeve is cut slightly larger than the tray on every dimension — usually 1.5–2.5 mm of clearance on the width and height, and 3–5 mm on the length so the tray slides without binding. Too tight and the tray jams; too loose and it rattles. At CKT we lock these clearances in the die layout and verify them on the first sample before wrapping.
1.1 V-Grooving Mitered Corners
Each greyboard panel is V-grooved at the fold lines so the wrapped corners fold crisply without bulging. The groove depth is set to leave about 0.3–0.4 mm of greyboard, which is enough to hold the corner square but thin enough that the wrapped paper does not crack.
2. Textured Paper Wrapping: Navy Speciality Paper at 120–140 gsm
The greyboard is wrapped with a printed and decorated specialty paper — here a deep navy paper with a subtle crocodile-emboss texture at about 130 gsm. The wrapping is done on rigid box assembly machines: glue is applied to the greyboard, the paper is positioned, and the four side flaps are folded in sequence.
Wrapping quality is judged by three things: no visible glue squeeze-out on the edges, corners that meet cleanly without a gap, and no bubble or lift on large flat areas. On textured papers, the emboss must align across the sleeve and tray so the pattern continues visually when the drawer is closed.
3. Print and Decoration: Five Processes on One Box Face
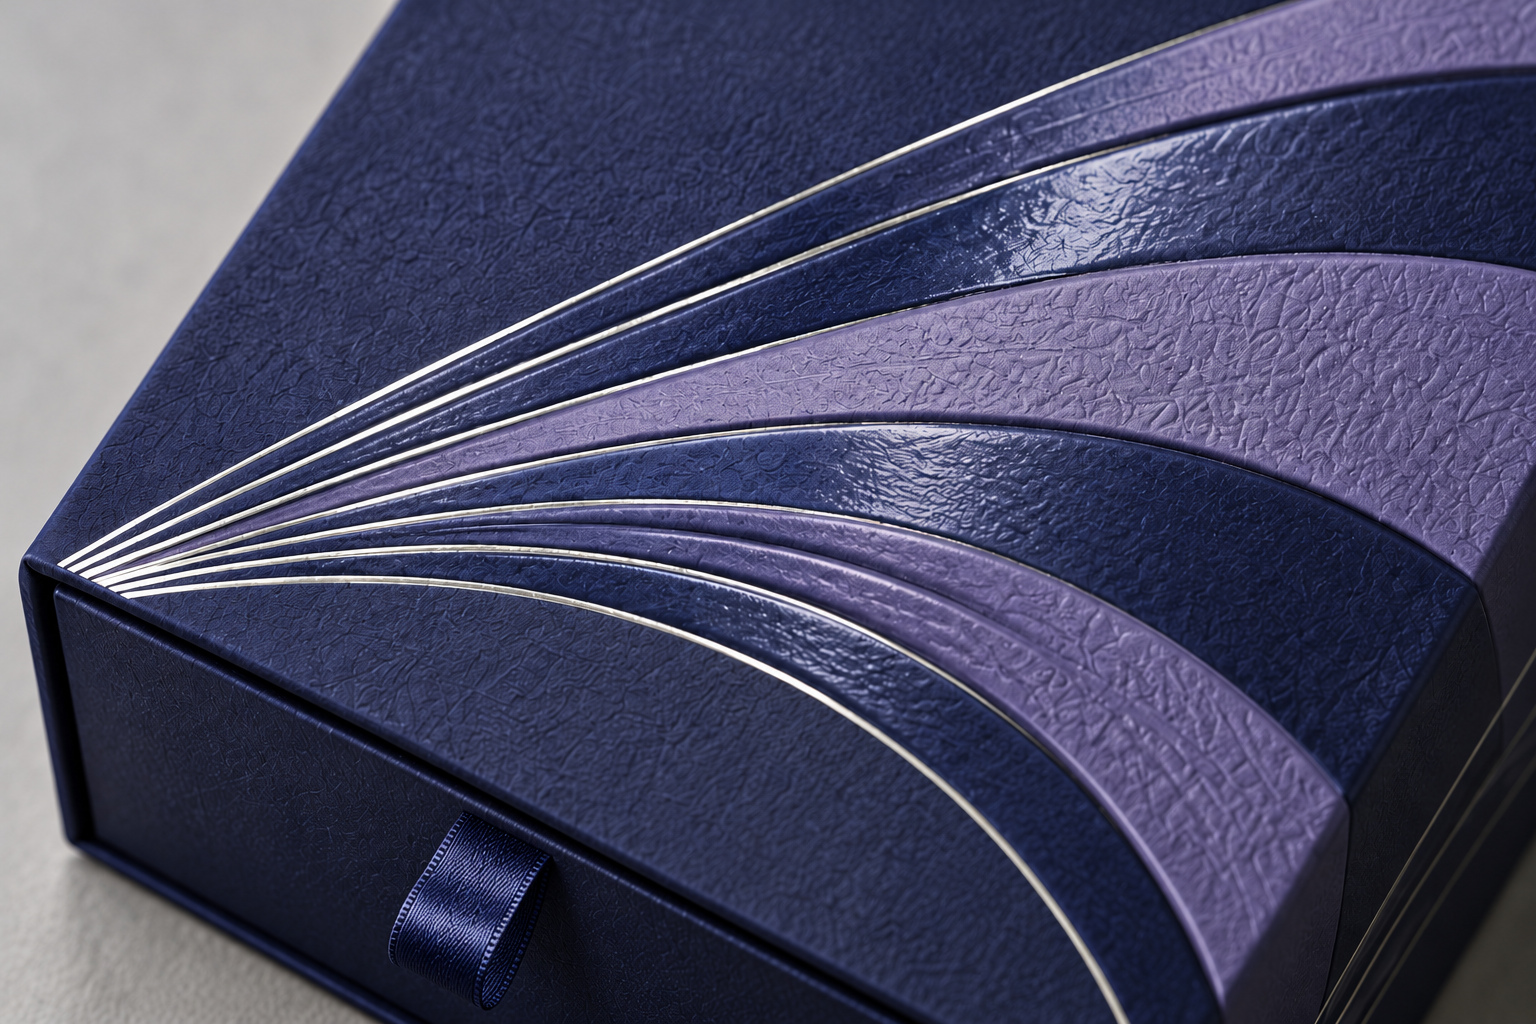
Close-up: purple fan offset print with emboss, silver foil lines, and spot UV on the navy fan zones.
The box face carries five decoration layers, and the sequence matters:
Offset printing: purple fan shapes printed as a spot colour over the navy paper. Because the paper is dark, the purple is printed with an under-base to reach the target hue.
Blind emboss: the purple fan areas are embossed against a textured die, giving a raised tactile surface without adding ink.
Silver hot foil: thin arc lines running from the lower-left corner are foil-stamped with a matte silver foil. Foil is applied after printing so the lines sit on top of the ink.
Spot UV: the navy fan zones receive a glossy UV varnish, creating a contrast with the matte surrounding paper.
Texture lamination: the base paper already carries a fine emboss, which is preserved through the print and foil stages.
Running five processes on one flat sheet requires tight registration: the emboss die, foil block and UV screen must all align within ±0.2 mm across the run. We check registration at the start of every shift and pull samples every 500 pieces.
4. Assembly: Tray, Sleeve and Ribbon Pull
Sleeve and tray separated — the tray interior is lined with off-white cardstock; the ribbon pull is anchored at the drawer front.
After wrapping, the sleeve and tray are assembled. The ribbon pull — here a navy grosgrain ribbon about 10 mm wide — is glued to the inside front wall of the tray, then folded over the front edge so it protrudes as a pull tab. The ribbon length is set so the tray slides out about two-thirds of its travel before the ribbon stops it.
The tray interior is lined with off-white cardstock to cover the greyboard edges and give a clean base for the bottle insert (when specified). For a 50 ml bottle, the insert cavity is sized to the bottle base, with about 0.5 mm clearance on each side.
5. QC and Batch Consistency
Before cartoning, each batch goes through:
Dimensional check: sleeve and tray measured with digital calipers at the start and end of the run.
Slide test: the tray is pulled open and closed 10 times on sample units — it should move smoothly without binding or falling out.
Decoration check: foil adhesion tape test, UV surface check, emboss depth visual check.
Colour check: navy and purple compared against the approved standard under D65 lighting; delta E is kept within tolerance.
CKT runs monthly capacity in the high-tens of thousands of rigid boxes across sleeve, magnetic lid, lid-and-base and drawer styles, with sampling AQL 2.5 on critical dimensions.
6. Why Drawer Boxes Are Growing in Men's Fragrance
Search data on Alibaba shows the term "luxury drawer perfume box" rising sharply in 2026, alongside growth in rigid perfume box keywords. Men's fragrance lines in particular are moving from simple folding cartons to drawer or magnetic boxes because the unboxing motion — pulling the ribbon, sliding the tray — adds a tactile moment that a tuck-end carton cannot.
For European brands, the box is also PPWR-ready: FSC-certified paperboard, mono-material inserts, no PVC, and any magnets specified as a separable component (not used on this ribbon-pull design).
7. Ordering: What We Need to Quote
To build a drawer box like this, share: bottle dimensions (base and height), target quantity, paper or colour references, and the decoration processes you want (foil, emboss, UV). We return a digital sample photo within 3–5 working days and a physical sample within 7–10 days. Production lead time is 25–35 days for first orders, depending on complexity.
Contact Shenzhen CKT Print Co., Ltd.
For custom rigid drawer boxes and long-term fragrance packaging programmes, contact our team:
Contact: Sherry Wu
Mobile / WhatsApp: +86 15815525889
Email: info@cktprint.com
Website: www.cktprint.com
Alibaba Store: https://cktprint.en.alibaba.com/
Factory Address: 2-3F, Building 3, Zhong Xin Industry Area, No.8 Yuhu Road, Fenggang Town, Dongguan City, Guangdong, PRC.

 Your message must be between 20-3,000 characters!